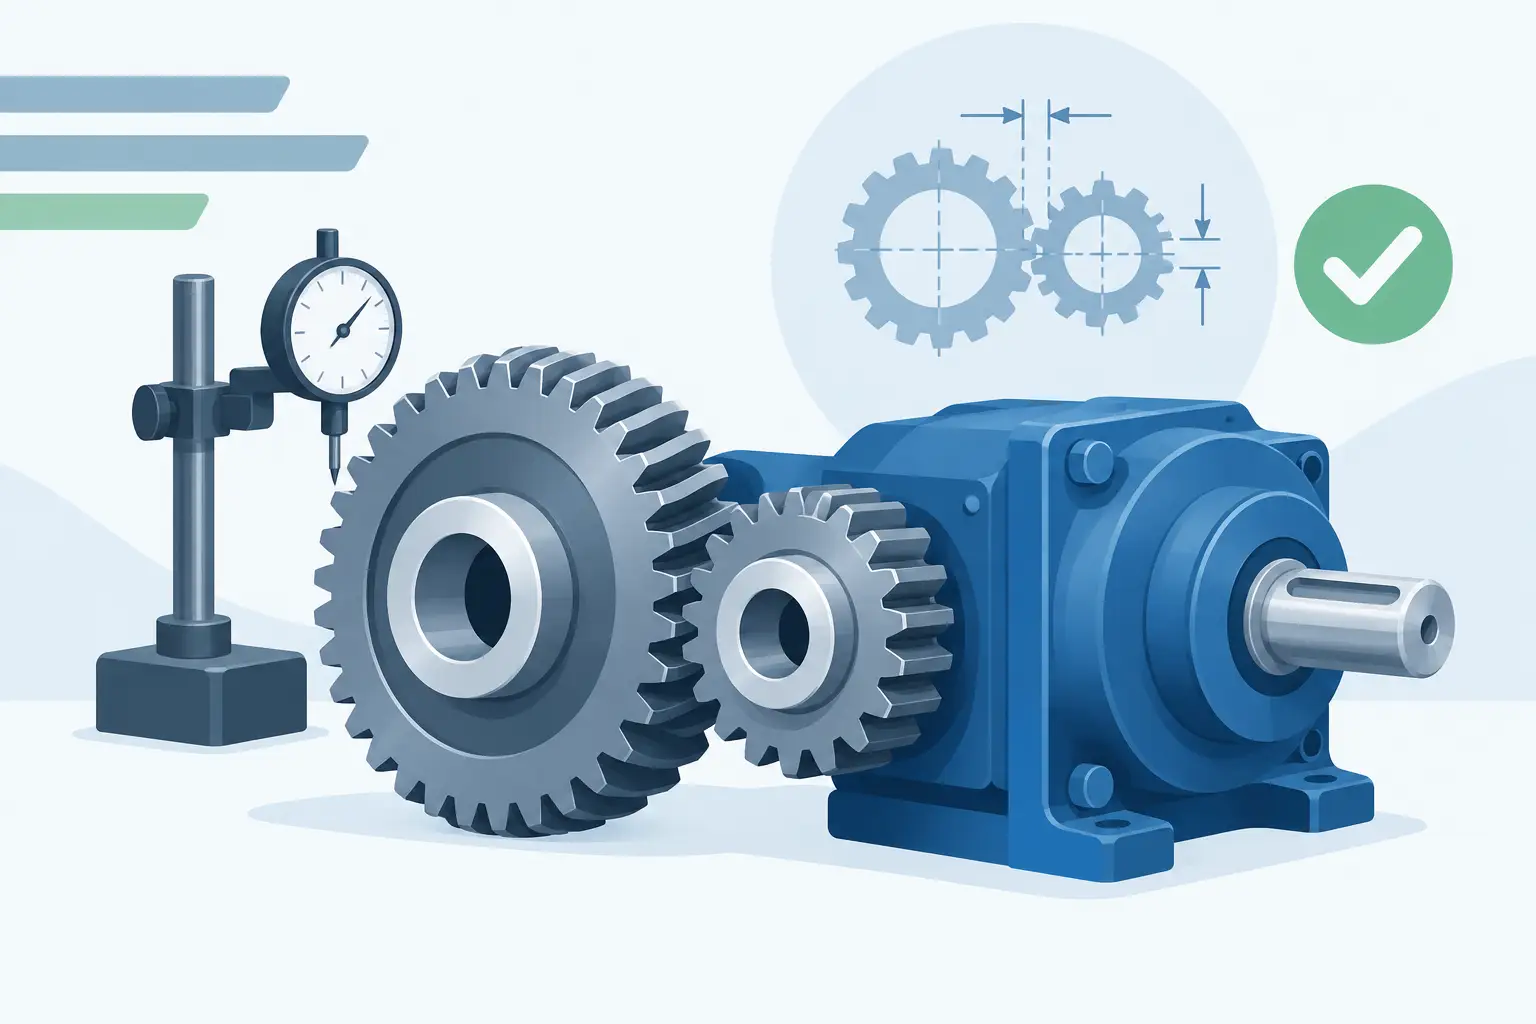
A gear pair can have the correct module, pressure angle and ratio, then still run noisily, bind at one point in the rotation, or load its bearings harder than expected. The difference is often not the nominal geometry. It is the permitted deviation from it. Gear tolerance standards turn that deviation into a specification that a manufacturer can measure, inspect and price.
For a prototype built on a benchtop machine, an unnecessarily tight quality class can consume budget without improving the mechanism. For a compact reducer operating at speed, a vague requirement can produce a gearset that meshes on paper but disappoints in service. The engineering task is to specify the quality needed by the assembly, not the highest number available on an inspection report.
What gear tolerance standards actually control
Nominal gear geometry describes the ideal involute tooth form. Tolerances define how far the real gear may depart from that ideal while remaining acceptable. They cover several distinct error sources, and those sources do not have the same effect on a mechanism.
Profile deviation concerns the involute shape along the tooth flank. A poor profile can concentrate load, reduce contact ratio and create transmission error. Lead deviation concerns the tooth direction across the face width. It matters particularly on helical gears, where incorrect lead or helix alignment can move load towards one end of the tooth.
Pitch deviation describes variation in the spacing of teeth. Single pitch error affects the spacing from one tooth to the next; cumulative pitch error builds across a sequence of teeth. These errors commonly appear as periodic speed variation, noise and inconsistent backlash around the rotation.
Runout, sometimes assessed through radial composite measurement, relates the tooth system to the gear datum axis. A gear can have a good involute profile yet run eccentrically because of bore, datum or blank errors. The result is a changing centre distance in operation, which changes backlash and can impose alternating loads on shafts and bearings.
Surface finish and material condition also influence noise, wear and load capacity, but they are not automatically covered by an accuracy grade. Neither are heat-treatment distortion limits, bore tolerances, shaft fits or bearing-seat requirements. A useful drawing or production specification keeps these requirements separate rather than expecting one gear-quality callout to control the whole part.
The standards behind gear quality grades
For metric cylindrical gears, ISO 1328 is a common reference. ISO 1328-1 addresses accuracy relevant to tooth flanks, including profile, lead and pitch-related deviations. ISO 1328-2 addresses radial composite deviations and runout. It gives designers and suppliers a shared system for selecting and verifying quality.
The ISO system works with defined quality grades, where lower grade numbers represent tighter permissible deviations. The exact allowable values depend on factors such as gear size, module and face width. A grade is therefore not a universal micron value, and it should never be copied between unrelated gear sizes without checking the standard tables.
AGMA accuracy systems are also widely used, especially where suppliers and inspection practices are aligned with North American specifications. AGMA quality levels and ISO quality grades are not labels to translate casually. Their measurement conventions, acceptance methods and nomenclature differ. If a supplier quotes AGMA, while the drawing calls up ISO, agree the governing standard and inspection basis before production starts.
Other standards define the geometry that sits underneath an accuracy requirement. ISO 21771 is relevant to cylindrical involute gear terminology and geometrical parameters. Material, heat treatment, load capacity and rating standards form another layer. They support a complete engineering decision, but they do not replace a manufacturing tolerance specification.
A grade is not a complete requirement
Saying that a gear must meet a particular quality grade is useful, but incomplete when the gear is part of an assembly. The grade must be tied to a standard, a gear type and an agreed inspection method. For a helical gear, state the relevant helix angle and hand. For a finished gear, clarify whether the quality applies after heat treatment and finishing, not only before.
The datum scheme is equally important. The inspection axis may be derived from the bore, journals or centres. If the tooth system is inspected relative to one datum but assembled relative to another, a compliant report can still hide an assembly problem. This is a common failure mode in compact gearboxes with short bearing spans.
Choose tolerance from the mechanism, not habit
A lightly loaded hand-operated mechanism can often tolerate wider tooth deviations than a high-speed motor drive. That does not mean low-cost gears should be specified carelessly. It means the limits should reflect the consequences of error: audible noise, positional repeatability, torque ripple, thermal load, service life and manufacturability.
Start with operating conditions. Rotational speed makes transmission error more audible. Torque and duty cycle make poor contact distribution more damaging. A wide face gear is more sensitive to shaft and housing deflection, so tighter lead accuracy alone may not solve an alignment problem. A plastic gear may need a different allowance for temperature, moisture and moulding variation than a steel gear.
Backlash deserves its own decision. Gear quality influences backlash variation, but it does not set the intended nominal backlash by itself. Backlash is determined by tooth thickness, centre distance, profile shift, assembly variation and thermal behaviour. A reducer that must reverse accurately may need controlled backlash and tight pitch variation. A drive expected to warm significantly may need more backlash, even when tooth accuracy is good.
The same distinction applies to centre distance. Tight centre-distance control can improve mesh consistency, but only if bearings, housings, shafts and mounting features can maintain it under load. Specifying premium gears in a flexible printed housing or thin sheet-metal enclosure is rarely an efficient route to low noise.
Match the specification to the manufacturing route
Manufacturing process sets a practical floor for gear quality and cost. Hobbing, shaping, milling, grinding, skiving, injection moulding and additive manufacture produce different error patterns. Post-processing, fixturing quality, heat treatment and final bore machining may matter as much as the tooth-cutting process.
For one-off prototypes, a CNC-milled gear may be fit for purpose at low speed, but should not be assumed equivalent to a production hobbed or ground gear. For additive manufacture, layer orientation, shrinkage, tooth-root condition and bore accuracy can dominate performance. It is sensible to validate mesh and packaging with printed parts, then specify a production route appropriate to the duty.
Avoid defining a tolerance that cannot be inspected economically. A specialist gear measuring machine can report profile, lead and pitch deviations in detail. A small shop may instead use composite checking, span measurement, over-pin measurement and functional mesh tests. None is inherently inferior if it verifies the critical requirement. The inspection plan needs to match the acceptance criterion.
Where noise is critical, ask for evidence that reflects the assembly. Single-flank rolling tests can reveal transmission error; double-flank composite tests are efficient for detecting combined variation and runout. A detailed tooth measurement report may still be worth requesting for a new supplier, a critical gearbox or a process change. For routine parts, functional inspection with controlled traceability may be the better commercial choice.
Build tolerances into the full drivetrain
A gear is not an isolated solid. Its quality only becomes useful when shaft shoulders locate bearings correctly, bearing fits suit the load and material, and the housing holds both axes where the design assumes they are. Small axial errors can reduce usable face contact. Radial clearance in a bearing arrangement can turn an acceptable no-load mesh into a noisy loaded mesh.
This is where parametric assembly geometry earns its place. Configure the true involute gear pair first, then inspect the shaft, bore, bearing and housing interfaces together. Check root clearance, tip clearance, face overlap and access for assembly. Decisions stay visible when a module change affects not just the teeth, but the bearing envelope and the available housing wall thickness.
GearSuite supports that mechanism-level workflow by combining tooth geometry with shafts, bearings and manufacturable solids. The design still needs an explicit production specification, but early checks help prevent a common mistake: applying precision tolerances to gears after the surrounding assembly has already made precision impossible.
A practical specification workflow
Set the nominal tooth system first: module or normal module, tooth count, pressure angle, helix angle, face width, material and heat-treatment condition. Then define the intended operating centre distance and backlash range. Select an accuracy standard and grade that suit the speed, load, noise target and production method.
Next, place the quality requirement beside the features that establish assembly accuracy. Specify bore tolerance, datum references, allowable runout to the functional axis, shaft and bearing fits, and housing centre-distance tolerance. Finally, agree which measurements prove compliance and whether inspection occurs before or after finishing and heat treatment.
Do not over-specify every dimension. Put tight control where it protects mesh, location or load path. Leave non-functional features with sensible general tolerances. This keeps drawings readable and prevents suppliers from paying for precision that cannot improve the mechanism.
Before releasing production files, test the design against the errors that are most likely in its chosen process. A few tenths of a millimetre of housing movement may matter more than a refined tooth-profile requirement. Conversely, a high-speed gear pair may justify finer flank control even in a rigid machined housing.
Set the gear quality level early, then let the shafts, bearings, housing and inspection method prove that the assembly can hold it. That is how a tolerance standard becomes a buildable drive rather than a line of text on a drawing.