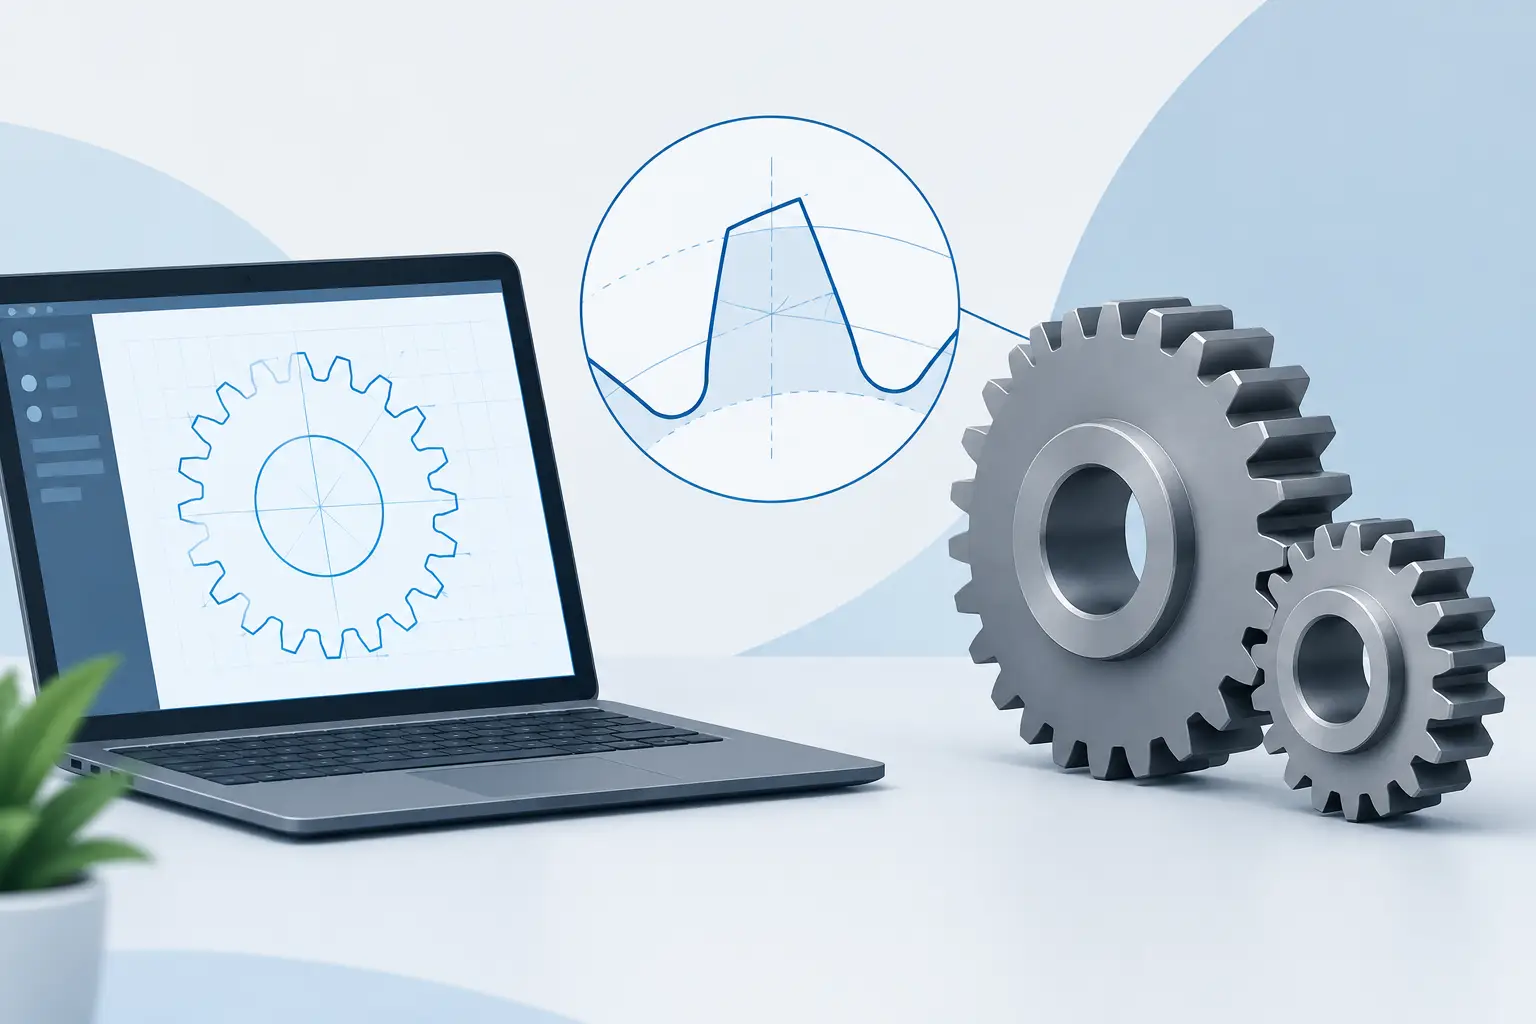
A gear tooth can look correct in a sketch and still fail where it matters: at the line of action, in the root, or when the mating gear reaches its intended centre distance. An involute gear profile generator exists to remove that uncertainty. It turns a small set of engineering inputs into tooth geometry that can transmit motion predictably, be inspected as an assembly, and move towards manufacture without rebuilding every curve in general-purpose CAD.
For makers and engineering teams, the value is not simply drawing a gear faster. It is keeping the decisions that define meshing performance visible from the first ratio calculation through to the exported solid.
What an involute gear profile generator must produce
An involute tooth profile is derived from the involute of a base circle. This geometry gives standard external gears a valuable property: within reasonable operating limits, a pair can tolerate small variation in centre distance while maintaining a constant velocity ratio. That is why involute systems dominate practical power transmission.
A useful generator must therefore do more than arrange repeated tooth shapes around a circle. It needs to construct geometry from the actual tooth system: module, tooth count, pressure angle, profile shift, backlash and face width. For helical gears, helix angle and handedness are equally fundamental. These parameters affect pitch diameters, addendum and dedendum diameters, base circles, tooth thickness and the way two gears contact one another.
A simplified gear outline may be adequate for an illustration, laser-cut prototype or low-load display mechanism. It is not adequate when a part must mesh smoothly, carry torque or sit on a shaft beside bearings and a housing. The distinction is straightforward: an involute generator should create engineering geometry, not a gear-shaped symbol.
The input values are connected
Module and tooth count establish the nominal pitch diameter. Pressure angle affects tooth form, contact behaviour and radial loading. A common 20-degree pressure angle is a sensible starting point for many applications, but it is not a universal answer. Existing systems, specialist applications and legacy components may use different standards.
Backlash is another example of a value that should not be treated as decoration. Too little can cause tight running when tolerances, thermal expansion, coating thickness or contamination are present. Too much increases positional error and can be unacceptable in indexing, robotics or reversing drives. The right setting depends on process capability, material, operating temperature and the function of the mechanism.
Profile shift deserves the same attention. It can help avoid undercut on low-tooth-count pinions, adjust centre distance or redistribute tooth strength across a pair. Applied carelessly, it can reduce the available addendum clearance or create a pair that no longer matches the intended assembly conditions.
Start with the mechanism, not the tooth outline
The practical workflow begins by defining what the transmission must do. Required speed reduction, torque, direction of rotation, available space, motor interface and shaft arrangement all influence gear selection. Choosing a tooth count pair before considering these constraints is a common source of rework.
For a simple spur pair, establish the ratio and choose tooth counts that meet it closely enough for the application. Then select a module appropriate to load, material and packaging. The calculated centre distance follows from the pitch diameters for a standard pair. If the available centre distance is fixed, profile shifts or a different tooth count combination may be needed.
Low tooth counts require particular care. A small pinion can be compact and useful for a high ratio, yet standard teeth may be undercut during generation. Undercut weakens the tooth root and changes the active involute portion. A capable generator should make this condition visible early, before the gear becomes a purchased blank or a printed part with a costly redesign ahead of it.
Helical gears add another layer. They can provide higher contact overlap and quieter engagement than spur gears, but they generate axial force. That force must be accommodated by suitable bearings, shaft shoulders, housings and retention features. A helical profile is not simply a spur tooth extruded at an angle. The normal module, transverse geometry and mating helix arrangement must agree.
Configure, inspect, validate, export
The strongest use of an involute gear profile generator is a disciplined four-stage workflow.
Configure the tooth system
Set the standards-based values first: module, pressure angle, tooth count and any profile shift. Define backlash deliberately rather than accepting a generic value. Add bore diameter, hub geometry, keyway or other shaft interface only after the tooth geometry is established.
This order matters because the gear is not an isolated component. A large bore may leave too little material at the root or hub. A hub that is convenient to model may clash with the mating gear, a bearing or a housing wall. Parameter-driven modelling keeps these dependencies visible.
Inspect the assembly geometry
A single gear can appear valid while the pair does not. Inspect both components at their intended centre distance and look beyond the pitch circles. Check root clearance, tip clearance, face overlap and potential interference with hubs or nearby parts.
A 3D assembly view is particularly useful when the drivetrain includes shafts, bearings and a housing. It exposes practical conflicts that a two-dimensional tooth plot cannot show. Exploded inspection also helps confirm that components can be assembled in the intended order, especially where press-fit bearings, retaining clips or recessed fasteners are involved.
Validate what the model is telling you
Engineering checks should guide decisions, not create false confidence. A warning about thin walls, unsuitable bearing fit, undercut or colliding solids needs a response in the design. Sometimes the solution is a larger module. Sometimes it is a longer centre distance, a different bearing series, a revised ratio or a change from a spur pair to a planetary arrangement.
The right answer depends on the duty cycle and manufacturing process. A lightly loaded PLA prototype can use choices that would be inappropriate for a machined steel reduction stage. Conversely, designing every bench-top mechanism around industrial margins can make it unnecessarily large and expensive. Useful validation makes the trade-off clear.
Export geometry that remains usable
The export format should match the next operation. DXF suits certain two-dimensional manufacturing routes and profile reference work. STL is practical for additive manufacturing and quick physical checks. STEP is generally the better handoff for machining, supplier review and integration with a wider mechanical assembly.
Export quality is more than file availability. The solid should include the intended bore, hub, face width and other production features, with geometry that remains coherent in downstream CAD or CAM. If shafts, bearings and housing interfaces were part of the design decision, they should not become disconnected assumptions at export.
Where basic gear calculators fall short
A ratio calculator can tell you that 12 and 48 teeth produce 4:1 reduction. It cannot establish whether the 12-tooth pinion is suitable, whether its bore leaves adequate root material, whether the bearing locations fit the shaft, or whether the housing can accommodate the resulting diameter.
Generic CAD can model those details, but it asks the engineer to build the tooth system, repeat features, mates, interfaces and checks from separate tools. That is reasonable for unconventional geometry or a fully bespoke machine. For standard gear mechanisms, it is often wasted effort.
GearSuite is designed around the missing middle ground: true involute gear pairs and transmission systems configured as connected mechanism geometry. Tooth profiles, shafts, bearings, housings and exportable solids remain part of the same working model. Decisions stay visible.
Manufacturing still sets the final limits
Generated geometry is the starting point for a manufacturable gear, not a substitute for process knowledge. FDM printing may require additional backlash, orientation changes and attention to layer direction at the tooth root. Resin printing can achieve finer tooth detail but brings different concerns around brittleness, post-curing and dimensional compensation.
For CNC machining, cutter access, internal corner radii, stock size and inspection strategy matter. For moulded, sintered or cut gears, material shrinkage, tooling constraints and finish requirements influence the final tooth system. If a gear operates at meaningful load or speed, consider lubrication, heat, noise, fatigue and the stiffness of the shafts and housing alongside the nominal profile.
The useful question is not whether a generator can produce a gear in seconds. It is whether the generated gear gives you a defensible next decision: change the module, alter the pinion, revise the bearing arrangement, or export the part with confidence. That is where a gear profile becomes a mechanism ready to build.